Application-Tested Handling
Product transfer and pack formation are confirmed around representative samples.
Conveying Systems
A configurable conveyor family for product transfer, accumulation, elevation and production-line balancing, designed around the product and factory layout.
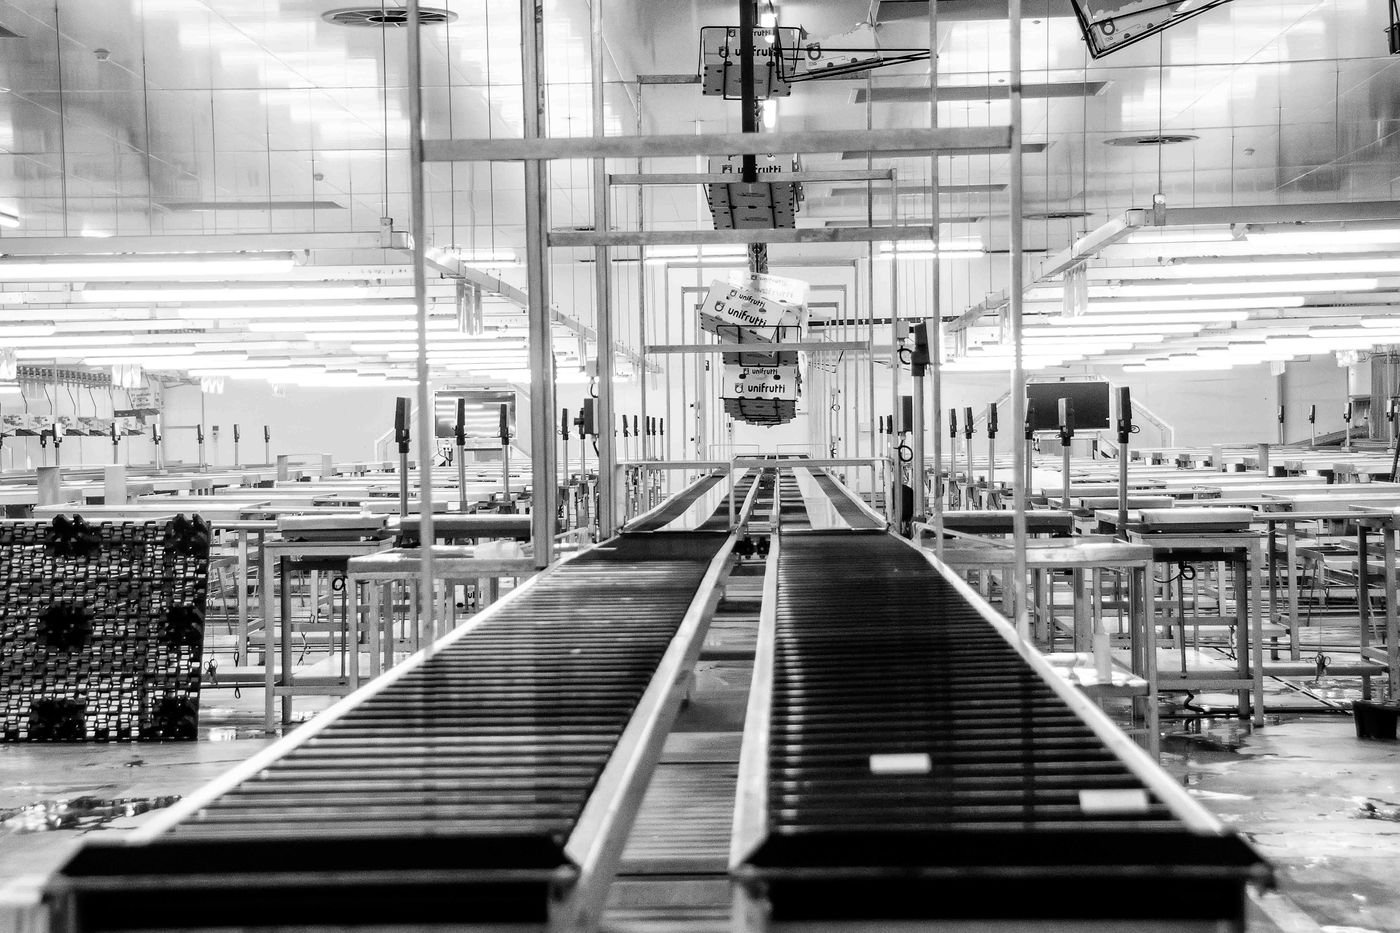
Series MC-200
A configurable conveyor family for product transfer, accumulation, elevation and production-line balancing, designed around the product and factory layout.
Product transfer and pack formation are confirmed around representative samples.
Stored settings and guided adjustments support multiple product formats.
Signals, transfer heights and accumulation logic are defined with adjacent equipment.
Electrical standards, documentation and commissioning scope can be adapted by market.
Equipment Snapshot
Demonstration figures show how a professional equipment page can present the operating range without hiding project-dependent conditions.
Selected by product and environment.
Custom elevations and transfers available.
Zone logic based on product pressure tolerance.
Line handshakes and status reporting available.
Equipment Overview
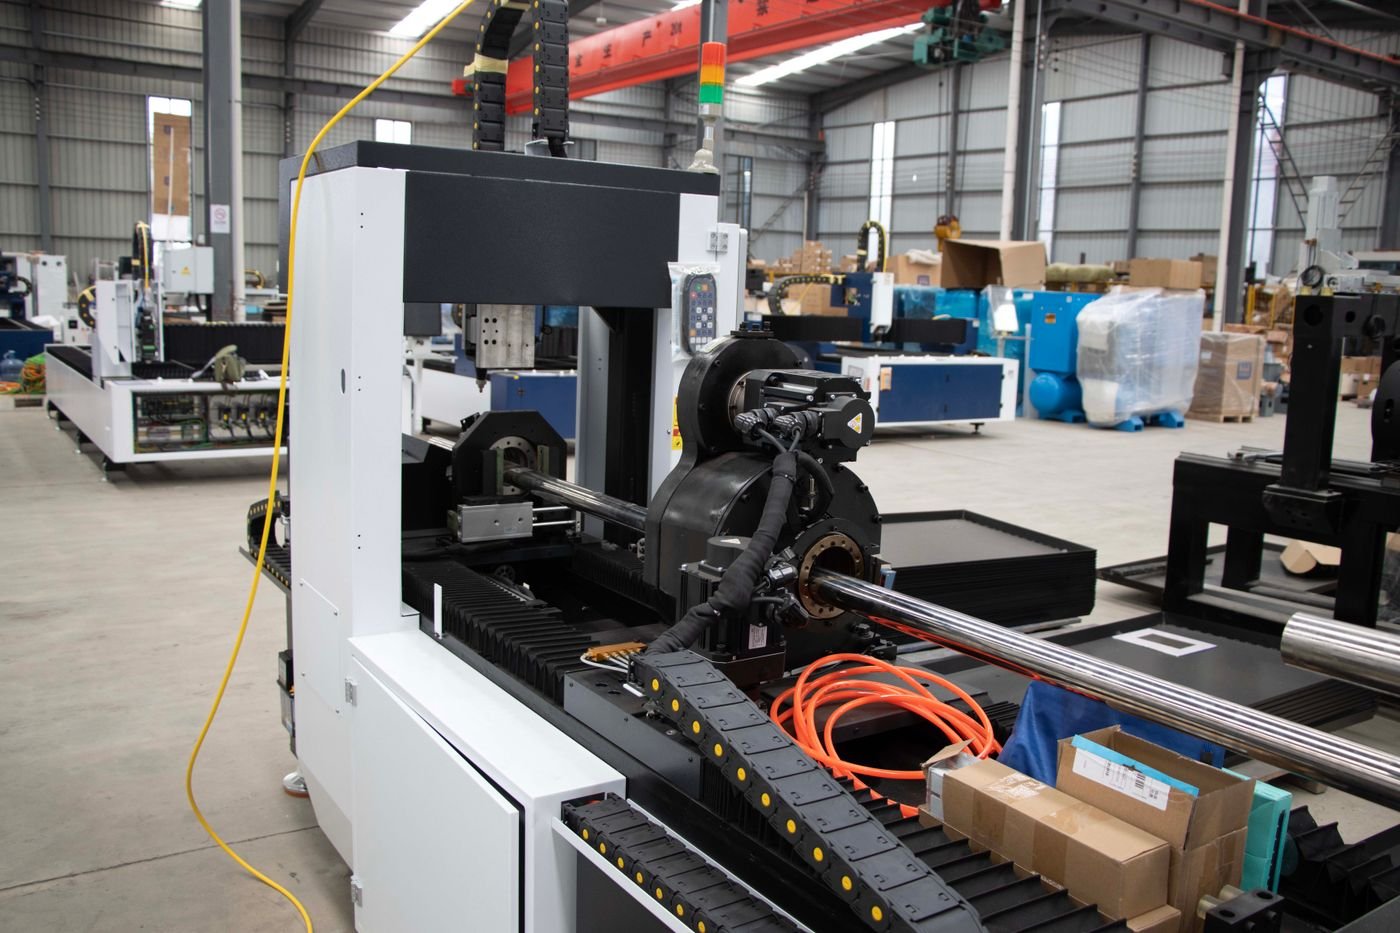
The MC-200 family includes belt, modular-chain and roller conveyor sections for straight transfer, curves, inclines, declines and controlled accumulation. Each section is selected around product contact, load, speed, cleaning, access and the surrounding equipment.
A conveyor project is more than a drawing of horizontal lines. Transfer gaps, guide geometry, support spacing, drive location, maintenance access and control zones determine whether the material flow remains stable.
The system can operate as independent sections or as a coordinated line with zone control, upstream and downstream handshakes, production status and fault management.
Technical Specifications
Final values are confirmed after sample, layout, utility and interface review. Each row can include an explanatory note instead of presenting isolated numbers.
Includes guide clearance and format range.
Line balance and product stability determine speed range.
Contact material selected for load and cleaning.
Selected for environment and load.
Profile and support depend on product geometry.
Location selected for access and transfer design.
Used for accumulation and line balancing.
Leveling range and anchors are defined in layout.
Project Advantages
These benefits come from application review, defined interfaces and measurable acceptance criteria rather than decorative feature claims.
Belt, guide and gap geometry are selected around the actual contact points and stability limits.
Accumulation and release logic reduce unnecessary stops between machines with different cycle behavior.
Drive access, cleaning clearance, removable guides and service zones are considered during layout review.
Sections can begin as standalone equipment and later connect to line-level status and recipes.
Typical Applications
Application suitability is confirmed against real samples, speed and environmental conditions before the final machine configuration is released.
Stable transport between filling, labeling, packing and inspection equipment.
Controlled product storage to balance short machine interruptions.
Incline, decline, spiral or lift interfaces where floor space is limited.
Case, pallet and wrapper conveyors with status handshakes.
Configuration & Integration
A complete quotation identifies what the machine receives, what it delivers and which functions belong to adjacent equipment or the customer site.
Transfer height, product orientation, access, guarding and installation clearances.
Power, safety, run permission, fault status, speed references and network connections.
Samples, utilities, local work, lifting, installation, validation and site acceptance responsibilities.
Operating Sequence
Each zone has a defined transfer purpose, speed relationship and response to downstream availability.
The product is accepted from upstream equipment at the defined height, speed and orientation.
Belt, guides and supports maintain stability through straight sections and direction changes.
Sensors and drives start, stop or release products according to downstream demand.
Products buffer with controlled pressure or zero-pressure separation where required.
The product leaves at the agreed position, spacing and signal condition.
Configuration Comparison
Use the same comparison factors when evaluating competing technical proposals.
| Selection Factor | PVC / PU Belt | Modular Plastic | Powered Roller |
|---|---|---|---|
| Best for | Small products and general transfer | Curves, washdown and robust handling | Cartons, totes and accumulation |
| Product contact | Continuous flat surface | Linked plastic modules | Individual rollers |
| Curves | Special belt or separate section | Flexible curved layouts | Curved roller sections |
| Cleaning | Material dependent | Open structure options | Best for dry logistics |
| Accumulation | Limited by product pressure | Possible with selected chain | Strong zone-control options |
Technical Review
Each tab answers a different procurement question and demonstrates a deeper product-content structure.
Dimensions, base shape, weight, softness, center of gravity and allowable back pressure determine the belt, guides and transfer details.
Scaled layouts include equipment footprints, columns, aisles, drains, maintenance zones and realistic transfer points.
Buffer length, zone size, release logic and allowable product contact are selected around real stop durations and line behavior.
Run permission, fault status, blocked conditions, speed references and line-stop philosophy are documented for every interface.
Drive location, belt replacement, guide removal, cleaning and spare-parts standardization are considered before fabrication.
Factory Acceptance Testing
Testing uses agreed samples, functions and acceptance methods. Project-dependent items are recorded rather than hidden.
Verify section lengths, transfer heights, supports and maintenance clearances.
Run minimum and maximum products through joints, curves and guide transitions.
Simulate downstream stops and confirm release order and product condition.
Check run permissions, faults, blocked status and restart behavior.
Inspect operating noise, guarding, cleaning access and service points.
Procurement Risk Review
A professional product page should make risk and project assumptions visible, not only list attractive features.
Rated speed is quoted without product and operating assumptions.
Tie output to approved samples, format, buffer condition, reject logic and FAT method.
Machine boundaries and adjacent-equipment responsibilities are unclear.
Approve a layout, interface list and responsibility matrix before manufacturing.
Installation and ramp-up support are discussed after shipment.
Define site readiness, commissioning, training, spares and remote support in the project scope.
Project Documents
These demonstration resources show how an independent site can present technical depth and reduce uncertainty before inquiry.
Equipment FAQ
The answers identify what must be confirmed during technical review instead of presenting unsupported guarantees.
The decision depends on product base, weight, stability, cleaning, accumulation and required curves. A product sample and layout are more useful than selecting by belt material alone.
Buffer length should be based on expected stop duration, line speed, product pitch and allowable pressure. The control philosophy is reviewed together with physical length.
Yes. Curved, incline, decline and lift solutions can be combined, subject to product stability and available footprint.
Yes. We need transfer heights, product exit conditions, available signals, speed ranges and maintenance access around the existing equipment.
Sections may run continuously, follow a speed reference or use sensor-based zones. The line-stop and restart behavior is defined in the interface list.
Typical documents include general arrangement drawings, electrical diagrams, component lists, manuals, lubrication information and recommended spare parts.
Related Equipment
Review upstream, downstream and complementary equipment using the same structured product system.
Buyer Resources
Long-form selection guides help buyers prepare better inputs, evaluate suppliers and define acceptance criteria.
Request a Technical Proposal
Attach representative product photos, drawings, packaging information or a short production video. The first response should identify missing technical inputs and a practical next step.